

 English
 Español
 عربى


Better Fastener Industry Co., Ltd. manufactures Rolling Screws alongside our broader screw, bolt, nut and washer programs. Founded in 2001 as a washer factory and expanded in 2010 into a comprehensive fastener enterprise, we produce thread-forming fasteners for aluminum die-cast housings, thin-wall zinc components and thermoplastic enclosures where thread reliability and swarf-free assembly matter.
Our rolling screw range follows DIN 7500 and TAPTITE-equivalent thread-forming geometry, supplied in case-hardened steel and stainless steel, with head styles, drives and point forms matched to the mating material and driving equipment on your line.
How Rolling Screws Form Threads
Rolling screws use a lobular thread form that cold-displaces workpiece material instead of cutting it. The three-lobe profile concentrates driving pressure at discrete contact zones, plastically forming a full female thread in the substrate while keeping the material grain flow continuous through the thread form. Because no material is removed, there is no swarf to contaminate a housing, and the formed thread resists stripping better than a cut thread of the same size in aluminum, zinc die-cast and thermoplastic assemblies.
- Thread formation: lobular profile displaces material into a mating female thread rather than cutting it away.
- Strength: cold-formed threads in metal substrates are typically stronger than cut equivalents because root material is compressed and densified.
- Assembly cleanliness: no chips or swarf generated during driving, which suits sealed housings and electronic enclosures.
- Reusability: formed threads tolerate service disassembly and re-driving better than cut threads in soft alloys.
Our Rolling Screw Range
We supply the DIN 7500 head and drive variants below, plus ASME inch-series thread-forming screws. Each item is produced to the referenced standard and can be adjusted for length, thread size, material and finish within the limits of the forming geometry.
| Designation | Head / Drive | Typical Fit |
|---|---|---|
| DIN 7500 (AE):2000 | Socket head cap, slotted | Recessed or counterbored metal housings |
| DIN 7500 (CE):2007 | Pan head, Phillips | General enclosure and panel assembly |
| DIN 7500 (ME):2000 | Countersunk head, Phillips | Flush surfaces in castings and sheet |
| DIN 7500 (NE):2009 | Oval countersunk head, Phillips | Trimmed panels and visible fixings |
| DIN 7500 (EE):2007 | Socket head cap, hex socket triangular | High-torque drives in structural castings |
| DIN 7500 (PE):2009 | Pan head, Torx triangular | Automated driving with cam-out control |
| DIN 7500 (DE):2007 | Hex head, triangular thread | Wrench-tightened joints in soft alloys |
| ASME B18.6.4:1998 | Truss head, Phillips | Inch-series sheet and light-gauge assemblies |
Application Fit by Substrate
Rolling screws are selected against the mating material first, then the head and drive. The table below maps the common substrate conditions we quote against to the forming behaviour that governs screw choice.
- Aluminum die-cast housings: formed threads resist stripping in thin bosses; pilot hole diameter is the critical variable.
- Thin-wall zinc components: lobular forming limits hoop stress compared with thread cutting in brittle castings.
- Thermoplastic enclosures: forming screws suit repeated service access where a moulded-in insert is not practical.
- Sheet metal and light-gauge steel: thread-forming screws replace nuts and washers in single-sided assemblies.
Materials, Finishes and Specifications
We produce rolling screws in case-hardened steel and stainless steel. Case-hardened grades give a hard, wear-resistant thread flank over a tough core, which is the usual choice for high-volume driving into metal substrates. Stainless steel is supplied where corrosion resistance or non-magnetic behaviour is required.
- Thread-forming geometry to DIN 7500 and TAPTITE-equivalent profiles.
- Inch-series thread-forming screws to ASME B18.6.4.
- Surface finishes include zinc plating and other post-treatments handled in-house.
- Dimensional and mechanical characteristics verified against the referenced standard before shipment.
Driving, Tooling and Line Integration
Rolling screws are driven with standard power tools, but torque and speed settings differ from cutting screws because the forming action generates higher driving torque and heat at the joint. We match drive type to your tooling: Phillips for general assembly, Torx and hex socket triangular drives where cam-out control and higher torque transfer are needed on automated lines.
For automated driving, the drive recess, head geometry and point form are specified together so that bit engagement, feed and seating depth remain consistent across the batch. Where a joint uses a nut or washer, our Nuts and washer ranges can be supplied as a matched assembly.
Quality Control and Acceptance
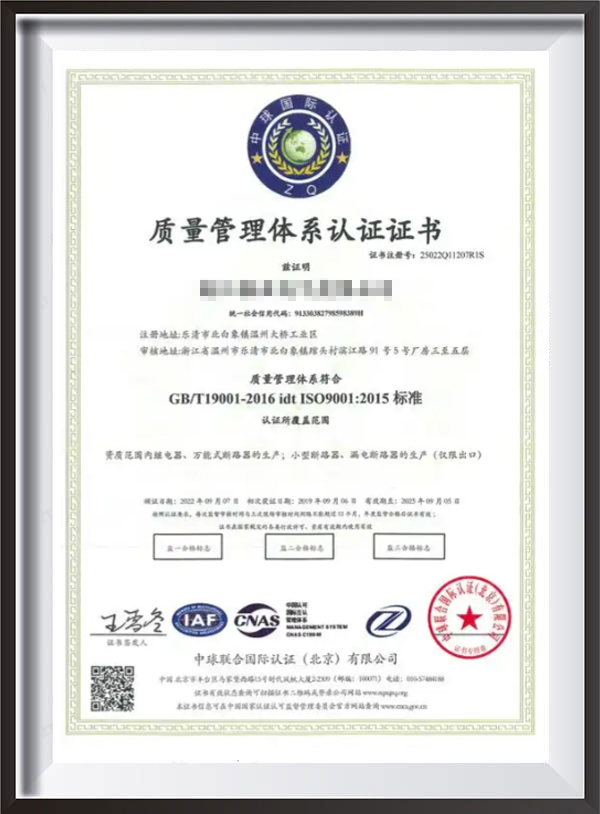
Our in-house laboratory and testing equipment support chemical composition, mechanical property, non-destructive and dimensional checks. Inspections are carried out after each production process, and finished products undergo final inspection against customer requirements and the referenced international standard. Our operations are certified to ISO 9001.
- Hardness and case depth verification on case-hardened items.
- Thread profile and dimensional inspection against DIN 7500 or ASME B18.6.4.
- Drive recess and head geometry checks for automated feeding.
- Documentation issued with the shipment as agreed at order stage.
Customization and Related Fasteners
Customized production is our core business. We develop rolling screws from drawings or samples, adjusting head form, drive, length, thread size, material and finish to suit the application. Where a project requires a different fastening principle, our Hexagon Flange Bolts and Bolts ranges cover bolted joints in the same assembly.
Information We Use to Configure Your Solution
To prepare a rolling screw configuration and quotation, we work from the joint rather than the part number alone. The following inputs let us confirm the forming geometry, material and finish in one pass.
| Input | Why It Matters |
|---|---|
| Mating material and grade | Sets the forming behaviour and the pilot hole range |
| Pilot hole diameter and boss wall thickness | Governs strip resistance and hoop stress in the boss |
| Thread size, length and head style | Defines the standard variant and any length adjustment |
| Drive type and driving tool | Matches bit engagement and torque transfer on the line |
| Material and finish | Confirms corrosion class and post-treatment |
| Annual volume and batch pattern | Aligns production scheduling and packaging scope |
| Inspection and documentation requirements | Defines the acceptance record issued with the order |
Packaging, Delivery and Serviceability
We consolidate rolling screws with the rest of a fastener program into one supply schedule, with retail kits, blister packs, custom boxes and export cartons available as packaging options. Our location within a two-hour drive of Shanghai and Ningbo ports supports sea freight as the main shipping mode, with air freight arranged for urgent deliveries.
Rolling screws are a consumable in service, so repeat orders are produced to the same drawing and inspection basis as the original batch. Spare and replacement quantities are quoted against the same specification so that line-side stock stays consistent.
Frequently Asked Questions
What is the difference between a rolling screw and a cutting tapping screw?
A rolling screw displaces material with a lobular thread form, while a cutting screw removes material. Rolling screws produce no swarf, form a denser female thread and resist stripping better in aluminum, zinc die-cast and thermoplastic assemblies.
Which standards do your rolling screws follow?
We produce DIN 7500 variants including AE, CE, ME, NE, EE, PE and DE types, plus ASME B18.6.4 inch-series thread-forming screws, in case-hardened steel and stainless steel.
Can you supply rolling screws to a drawing or sample?
Yes. Customized production is our core business, and we develop rolling screws from drawings or samples, adjusting head form, drive, length, thread size, material and finish.
How do you control quality on thread-forming screws?
Inspections run after each production process, with final inspection of finished products against customer requirements and the referenced standard. Our laboratory covers chemical composition, mechanical properties, non-destructive testing and dimensional checks, and our operations are certified to ISO 9001.
What information do you need to quote a rolling screw program?
Mating material and grade, pilot hole diameter, boss wall thickness, thread size, length, head style, drive type, driving tool, material and finish, annual volume and any inspection or documentation requirements.
Do you supply rolling screws together with other fasteners?
Yes. We consolidate rolling screws with bolts, nuts and washers into one specification-led supply program, with packaging and shipping arranged to match your delivery schedule.


